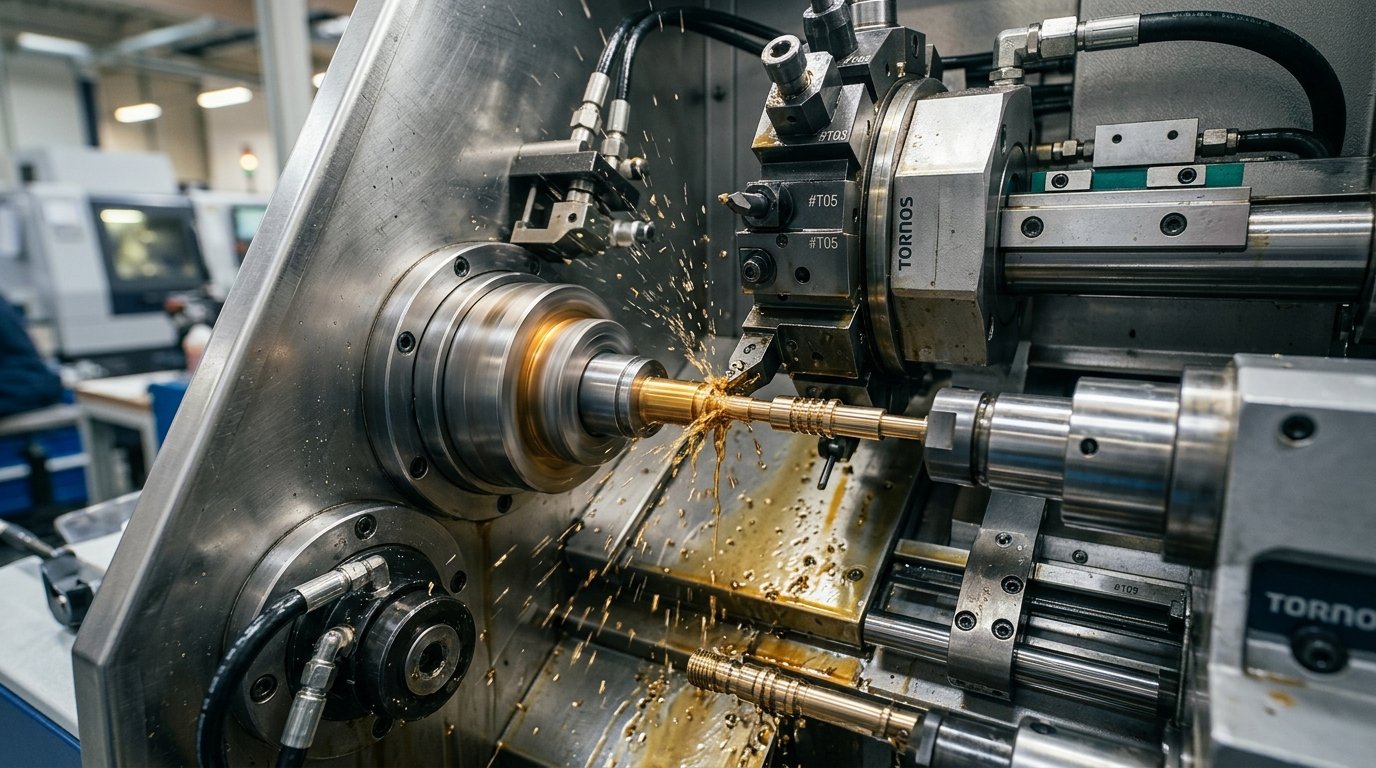
The Micron Imperative in Modern Precision Turning
In high-performance automotive assemblies, electrical switchgear, and medical instrumentation, micro-turned pins and threaded shafts are subjected to severe mechanical stresses and cyclic thermal loads. When component diameters fall between 1mm and 25mm, conventional fixed-headstock CNC turning often struggles with bar deflection and spindle chatter.
At Parwati Engineering Works, our Swiss-type sliding head automatic lathes and high-speed multi-axis turning centers eliminate workpiece deflection by supporting the raw stock directly at the cutting point with a synchronized guide bushing.
By moving the material along the Z-axis through a precision carbide guide bushing while the cutting tools remain stationary close to the support, cantilever overhang deflection is reduced to zero, enabling repeatable tolerances of ±0.005mm (5 microns).
Swiss Sliding Head vs. Conventional CNC Lathe Comparison
| Machining Parameter | Swiss Sliding Head Lathe | Conventional Fixed Head CNC | OEM Application Impact |
|---|---|---|---|
| Length-to-Diameter (L/D) Ratio | Up to 20:1 without tailstock | Limited to 3:1 to 4:1 before chatter | Ideal for slender shafts, connector pins & needle valves |
| Repeatable Tolerance Range | ±0.003 mm to ±0.008 mm | ±0.015 mm to ±0.025 mm | Eliminates secondary cylindrical grinding operations |
| Surface Roughness ($R_a$) | $R_a$ 0.2 to 0.4 μm | $R_a$ 0.8 to 1.6 μm | Superior sealing surface and wear resistance |
| Cycle Time for Micro Parts | Extremely rapid (sub-spindle overlap) | Moderate (sequential tool indexing) | Lower per-unit component procurement cost |
Key Factors in Achieving Zero Defect Micro-Turning
- Raw Material Homogeneity: Using drawn and ground bar stock (h8/h9 diameter tolerance) to ensure seamless sliding through guide bushings without binding.
- Coolant Temperature Stabilization: Utilizing high-pressure cutting oil with dedicated heat exchangers to eliminate thermal expansion drifts over 8-hour continuous shifts.
- Rigid Micro-Grain Carbide Tooling: Polished rake faces and precision corner radii prevent built-up edge (BUE) when machining sticky alloys like SS304 or high-copper brass.
Metrology and Optical Inspection
Sub-micrometer accuracy requires calibrated inspection. Every production batch at Parwati Engineering undergoes initial setup verification on digital optical profile projectors (shadowgraphs) and high-accuracy air gauging before batch sign-off.
Looking for Precision Turned Components?
Submit your component technical drawing or sample request to our engineering team for a same-day feasibility report and transparent quotation.
Request a Feasibility Quote →